
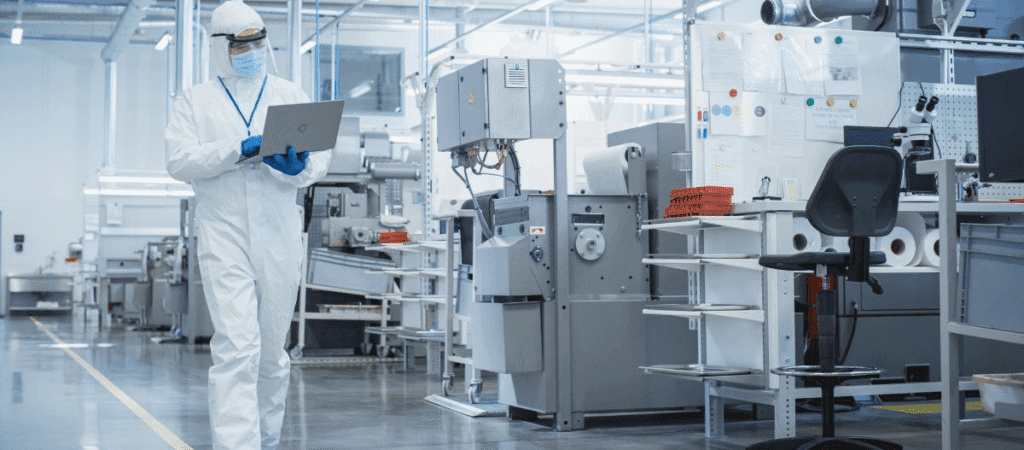
The design of Good Manufacturing Practice (GMP) compliant pharmaceutical manufacturing environments begins with a simple principle: production conditions should be matched to the contamination risks associated with the drug product and its packaging. The primary contamination risks for pharmaceutical products and packaging materials are microbial contamination and environmental particulate contamination, both of which can compromise product quality, reduce sterility assurance, trigger adverse reactions, and ultimately threaten patient safety.
The purpose of the ISO cleanroom classification system is to quantitatively control airborne particulate and microbial contamination by establishing manufacturing environments appropriate to the risk level of the pharmaceutical product. In general, higher-risk products, such as sterile injectable manufacturing, require higher cleanroom classifications than non-sterile products.
ISO Class 5: The Critical Barrier for Sterile Manufacturing
ISO Class 5 (corresponding to Grade A cleanroom in EU GMP) represents the highest level of environmental control for critical aseptic operations.
Typical environmental requirements include no more than 3,520 particles ≥0.5 μm per cubic meter of air, airborne microbial counts not exceeding 10 CFU/m³, and settle plate counts not exceeding 1 CFU per plate. A medical packaging manufacturer adhering to Grade A cleanroom standards safeguards product integrity and patient safety.
ISO Class 5 cleanrooms typically employ unidirectional (laminar) airflow at velocities of approximately 0.3–0.5 m/s, creating a continuous sterile air barrier that minimizes particle deposition and microbial ingress. Positive air pressure, generally at least 10 Pa above adjacent areas, prevents contaminated air from entering the critical zone.
Personnel are required to wear complete sterile garments and pass through multiple stages of gowning and disinfection before entry. These environments are used for high-risk operations such as aseptic filling, stoppering, and manufacturing of sterile injectable products.
ISO Class 7: Background Protection for Aseptic Operations
ISO Class 7 (typically corresponding to Grade B background areas) provides the controlled environment surrounding ISO Class 5 critical zones.
Under static conditions, particle concentrations of ≥0.5 μm are limited to 352,000 particles per cubic meter, while airborne microorganisms are limited to 100 CFU/m³. During operation, environmental conditions should continue to support the cleanliness required for adjacent critical processing areas.
ISO Class 7 cleanrooms generally use non-unidirectional airflow with at least 25 air changes per hour and maintain a pressure cascade of at least 5 Pa relative to surrounding areas. Personnel are required to wear sterile cleanroom garments and complete gowning and disinfection procedures before entry.
ISO Class 8: Basic Environmental Control for Supporting Operations
ISO Class 8 (generally corresponding to Grade C or D environments, depending on the process) provides basic contamination control for non-sterile manufacturing and supporting pharmaceutical operations.
Typical environmental limits include no more than 35,200,000 particles ≥0.5 μm per cubic meter and airborne microbial counts below 500 CFU/m³. These cleanrooms commonly utilize multi-stage filtration systems consisting of pre-filters, intermediate filters, and HEPA filters, together with a minimum of 15 air changes per hour.
Operators wear cleanroom garments and follow routine hand hygiene and gowning procedures before entering the production area. Regular environmental cleaning and microbial monitoring are essential to maintaining the required cleanliness level.
Cleanroom Requirements for TPE Co-Injection Euro Caps
TPE co-injection Euro Caps used in BFS and FFS cleanroom systems for large-volume parenteral (LVP) products are classified as high-risk pharmaceutical packaging components. Although these drug products typically undergo terminal sterilization, particulate contamination and microbial contamination introduced during packaging manufacture can still adversely affect product quality and may reduce the effectiveness of the sterilization process.
Modern TPE co-injection manufacturing, particularly for JSD Cap®, utilizes high-precision, multi-component injection molding technology with highly automated production. This manufacturing process can be operated within an ISO Class 8 cleanroom, while final product handling and packaging can be performed in an ISO Class 5 environment. Such levels of environmental control are difficult to achieve with conventional mechanically assembled combination caps that utilize thermoset rubber components.
Conclusion
ISO cleanroom classifications are more than environmental specifications—they are an integral part of pharmaceutical quality assurance. By controlling airborne particles and microbial contamination according to the risk level of the product, cleanroom systems help ensure the safety, sterility, and consistency of both pharmaceutical products and their packaging components. For high-risk applications like TPE co-injection Euro Caps used in LVP packaging within cleanrooms, advanced manufacturing under ISO-controlled cleanroom conditions with HEPA filtration systems provides an additional level of confidence that the finished product meets the stringent requirements of modern pharmaceutical production.
